Craftsmanship, Scale
& Vertical Production
With corporate presence in New York and vertically integrated manufacturing facilities, DODGEHELL is an integrated sportswear and athletic team uniforms manufacturer. For over two decades, our factory operations have supplied international sporting goods brands, professional sports clubs, collegiate programs, and private labels with export-ready game jerseys, custom match kits, and teamwear.
Vertical Integration. Direct Factory Export.
At DODGEHELL, we maintain complete oversight of the athletic uniform manufacturing lifecycle. From technical fabric testing and laser cutting to multi-line jersey stitching, sublimation pressing, tackle-twill embroidery, and team-sorted dispatch, our centralized operations guarantee consistency and pro-league durability.
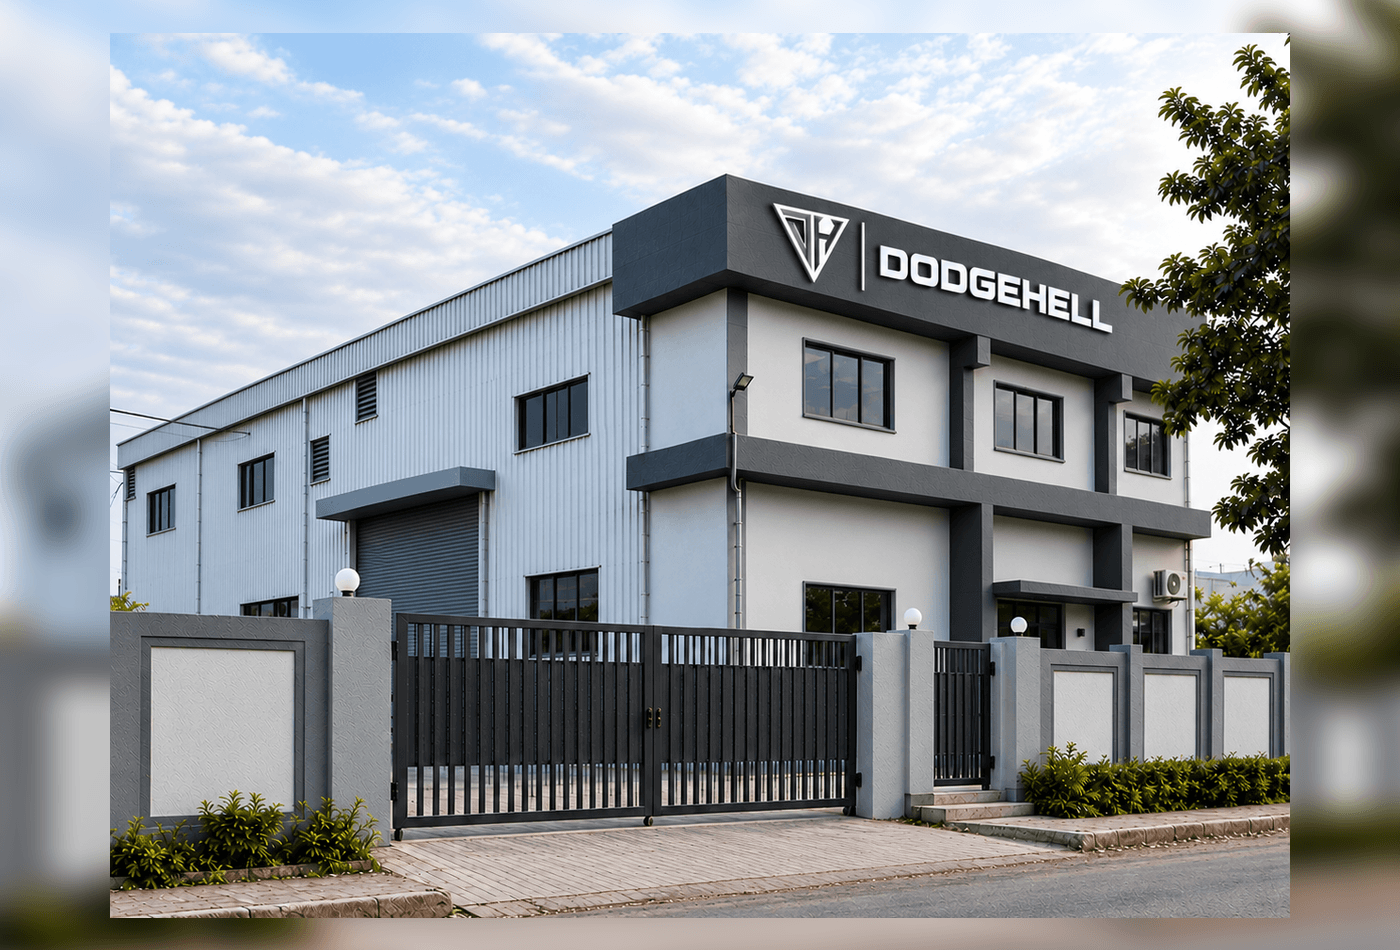
Vertically integrated technical sportswear, jersey & team uniform manufacturing facility
Scalable volume capacity across sports jerseys, teamwear uniforms, and athletic warmups
Standardized quality control systems and athletic apparel safety compliance
Direct teamwear shipments to athletic clubs, brands, and sports leagues worldwide
Inside Our Manufacturing Operations
Explore authentic views of our facility in action—from technical design formulation and fabric selection to precision assembly lines, rigorous AQL inspection, and global export packaging.

Uniform Engineering & Performance Fabric Selection
Every sportswear uniform order initiates with complete roster breakdowns, digital vector pattern drafting, and certified high-performance yarn selection. From 200 GSM diamond air-mesh for basketball jerseys and 300 GSM interlock for rugby, to heavy 4-way stretch spandex for football pants and lightweight aero-poly for soccer kits, our textile engineers test tensile burst strength, GSM weight, and 100% colorfastness before cutting.
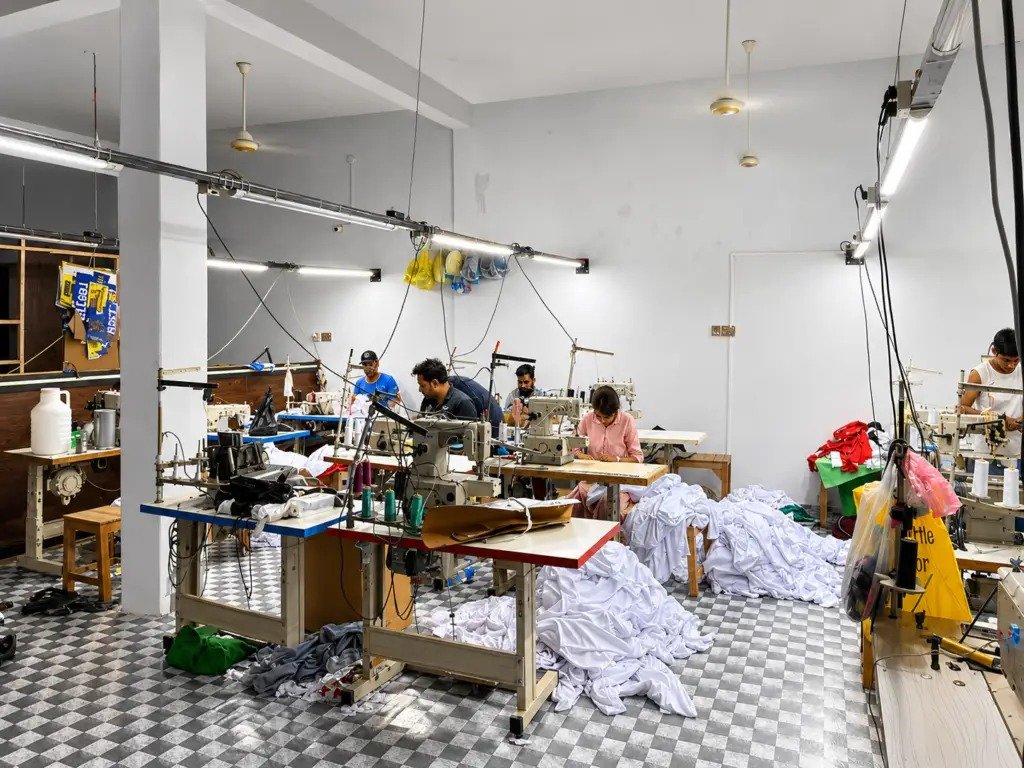
Precision Stitching Lines & Multi-Method Embellishment
Our high-capacity manufacturing floors feature specialized assembly lines engineered for team athletic uniforms. Equipped with 6-thread flatlock machines, heavy-duty coverstitch stations, automatic bar-tackers, and precision tackle-twill embroidery heads, each line is purpose-built for basketball jerseys, football game pants, baseball button-downs, soccer match kits, and team tracksuits.
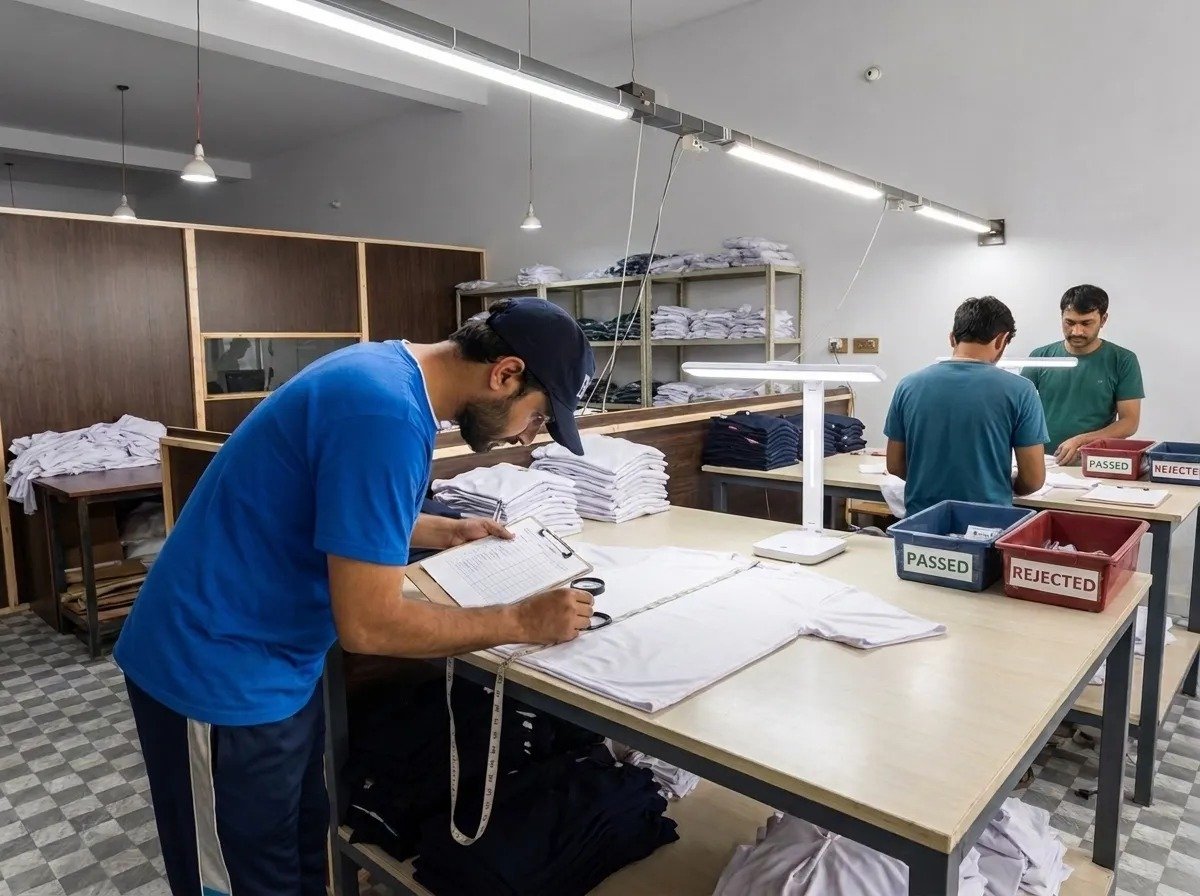
AQL 2.5 Quality Assurance & Roster Verification
Quality control is integrated at each workstation, backed by a dedicated QA team that verifies every uniform against the approved master roster sheet. Every jersey and short is audited for exact player name spelling, number placement, chest logo alignment, seam tensile strength, and colorfastness under high-temperature wash simulations.
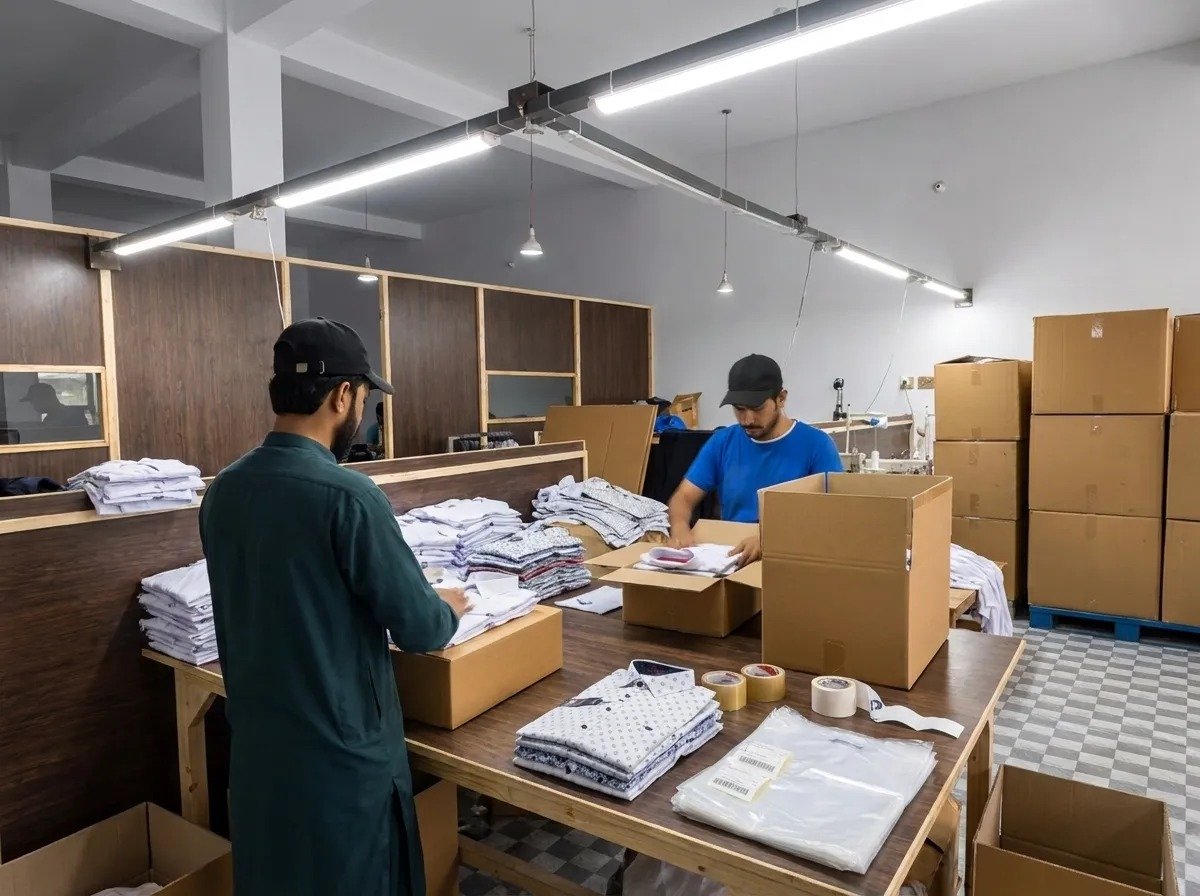
Team-Sorted Export Packaging & Worldwide Dispatch
Approved uniforms are steam-finished, individually polybagged with player names and size labels, and packed in team-sorted master cartons for effortless distribution by coaches and equipment managers. Shipments are dispatched with full tracking via priority air express or containerized ocean freight to athletic brands, leagues, and schools worldwide.
Why Sports Leagues & Brands Choose DODGEHELL
Direct factory contracts, clear wholesale volume tiers, and uncompromised athletic uniform craftsmanship.
100% In-House Facility Control
All jersey assembly, dye-sublimation, tackle twill, embroidery, roster numbering, and packing take place within our unified manufacturing facility.
Skilled Artisans & Ethical Standards
Fair compensation, clean and safe workplace conditions, zero child labor, and continuous technical training for our dedicated teamwear workforce.
Prototype Samples to Full Team Runs
Rapid turnaround on pre-production samples and fit prototypes, allowing athletic directors to verify fabrics, cuts, and finishes prior to full production.
Reliable Global Logistics (DDP / FOB)
Comprehensive export solutions including customs clearance, documentation, air express, and ocean container freight directly to your doorstep.
Begin Manufacturing with DODGEHELL
Submit your team roster or technical specification sheet to inspect our sublimation facilities, tackle twill stations, finished sample collections, and export packing operations.